The problem with hard water in boilers
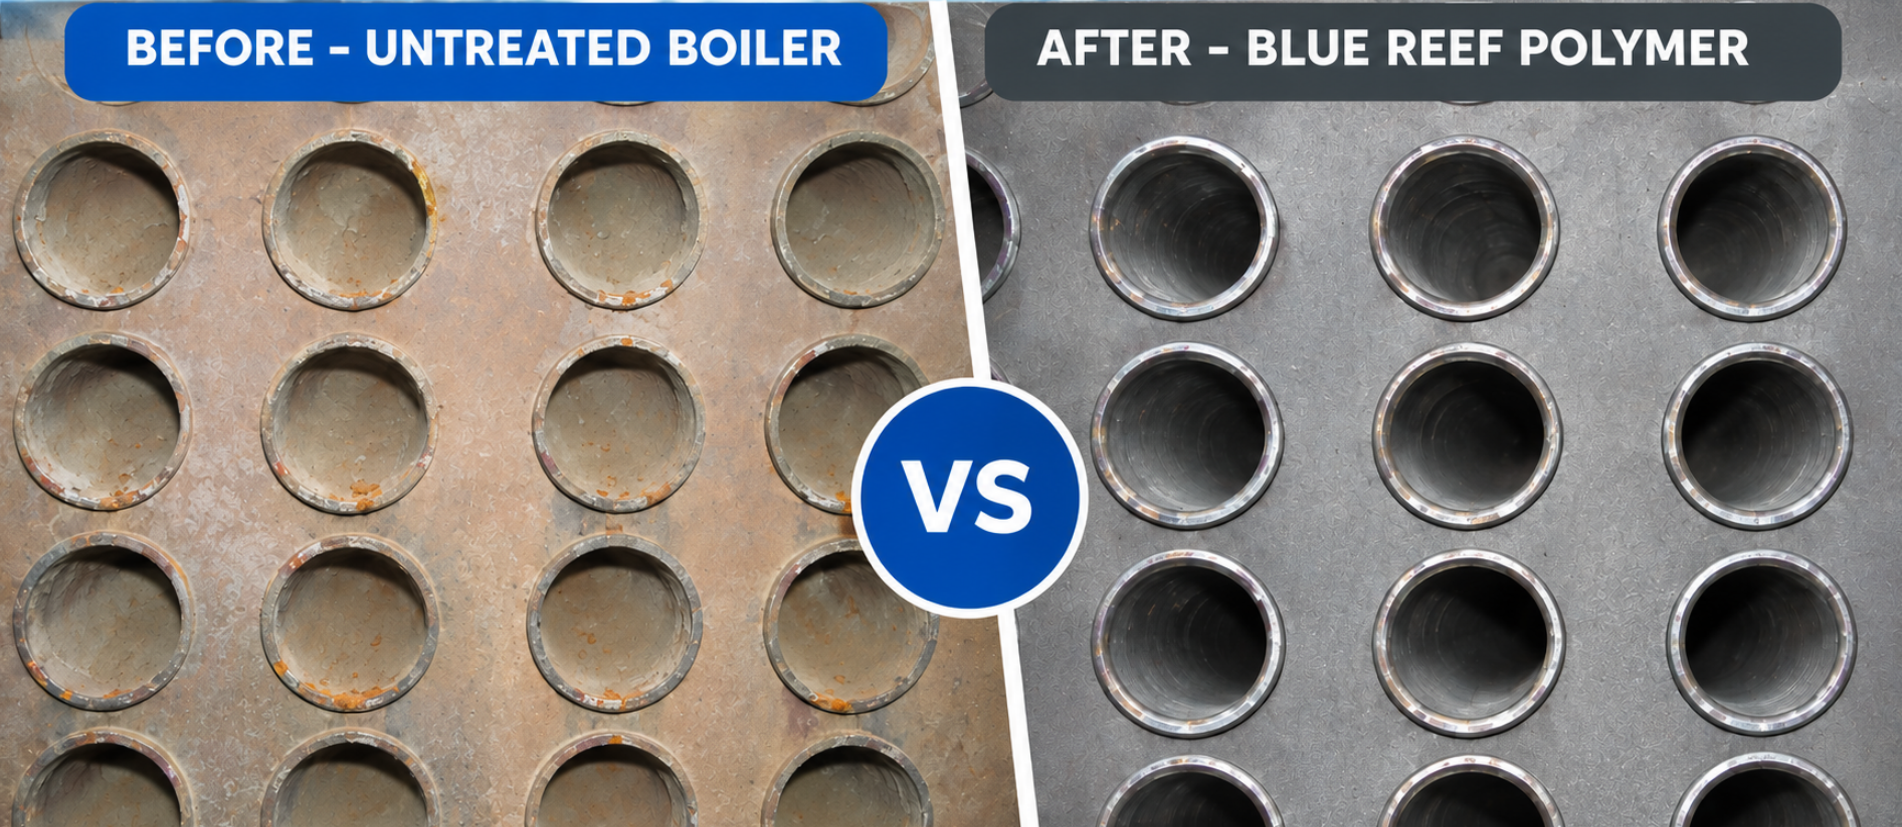
Raw and municipal water contains calcium and magnesium. When hard water in boilers is heated, these minerals come out of solution and settle on tubes and heat transfer surfaces. Even a thin layer of scale acts as insulation, so the boiler burns more fuel to produce the same amount of steam.
Over time, deposits can also contribute to boiler corrosion and tube damage. This is why the right boiler water treatment matters from day one.
How traditional phosphate treatment works
Conventional phosphate programmes control hardness through precipitation. Phosphate is added to the boiler, the calcium and magnesium precipitate out, and the solids stay suspended as boiler sludge. That sludge has to be removed through blowdown. More blowdown means more hot water leaves the system and must be replaced with cold make-up water, which then has to be heated. The result is higher energy use, higher fuel costs and higher water consumption.
A smarter approach: polymer boiler treatment
Blue Reef’s polymer boiler treatment works differently. Instead of precipitating hardness, our specialised polymers keep calcium and magnesium in solution and dispersed. They are carried out of the boiler without forming heavy sludge or hard scale.
This approach brings four clear benefits:
- Less blowdown. Less hot boiler water is lost, so less energy is needed to reheat make-up water.
- Water savings. Reduced blowdown helps lower overall water consumption and operating costs.
- Enhanced protection. It supports scale control and corrosion protection across heat transfer surfaces.
- Optimised performance. Stable, sub-stoichiometric technology allows precise, consistent control.
Boiler water treatment for every pressure range
- Low pressure (below 10 bar / 150 psi): basic protection against scale and corrosion, with polymer treatment recommended.
- Medium pressure (10 to 41 bar / 150 to 600 psi): greater concern for scale, deposits and oxygen pitting, where polymer programmes offer an advanced treatment approach.
- High pressure (above 41 bar / 600 psi): strict water chemistry control and advanced treatment for demanding environments.
Total protection across your boiler system
- BCI-L35-C: a concentrated bisulphite-based oxygen scavenger for corrosion control in steam generating systems.
- BST-L50-C: a food approved alkaline amine blend that neutralises carbon dioxide in the steam and condensate. It is also available in solid form as BST-S100-C.
- BIT-L50-HP: a specialised polymeric solubilising treatment designed to control and remove hardness deposits, organic foulants and metallic contaminants.